Hey there, if you’ve ever looked at a PP hollow sheet machine and wondered why some parts hold up for years while others wear out in months, you’re not alone. As a PP hollow sheet machine supplier who’s chatted with hundreds of manufacturers over the last decade, this question comes up all the time. It’s not just about “durability” — it’s about how much a part can handle the constant friction, heat, and polymer abuse that’s par for the course in making those lightweight, corrugated sheets you see in packaging, agriculture, or automotive trim. Let’s break this down like we would over a coffee at a trade show, no stuffy jargon — and definitely no AI-style fluff. PP Hollow Sheet Machine
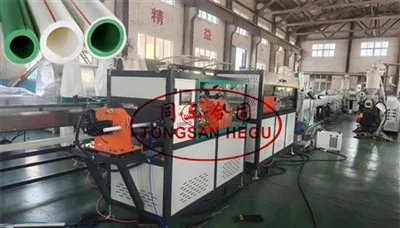
First, let’s get one thing straight: wear resistance here isn’t a one-size-fits-all number. A part that makes contact with molten PP (polypropylene) behaves way differently than one that rubs against the solid sheet as it’s being stretched and cut. I’ve seen clients skip this nuance, buy cheap generic parts, and end up shutting down production for repairs way more often than they should. That’s the first mistake to avoid.
Let’s start with the most worn-out parts most of our customers ask about: the extruder screws and barrels. These are the heart of the machine, right? They’re spinning at hundreds of RPM, shoving molten PP through a die, and the material itself is semi-molten, so it’s sticky and abrasive once it has any additives. Wait — most PP has fillers, like calcium carbonate, to cut costs. Those tiny calcium particles are like sandpaper inside the barrel. So wear resistance here isn’t just about the metal being hard — it’s about how well it can resist both abrasive particles and the chemical corrosion from molten PP (especially if it has UV stabilizers or other modifiers). Back in the day, we used to stock standard steel screws, but those only lasted 6-8 months. Now we offer two upgraded options: nitride-treated steel, which adds a super hard, thin surface layer, and bimetallic lined barrels, where the inner layer is a tungsten carbide alloy. The bimetallic ones? They run 2-3 years, easy. A lot of our clients laugh when they first see the price difference, but then they stop spending 2 days every other month replacing screws — that math adds up fast. I had a customer last year who switched from standard to bimetallic, and he told me his downtime dropped 70%. That’s the real win with wear resistance here.
Next up, the dies. The die is what shapes the molten PP into that hollow corrugated structure. The lips, the flow channels, the areas where the sheet pulls away from the die — all of these deal with both molten PP friction and solid sheet dragging along. Dies are usually made of tool steel, but the wear-resistant coating makes all the difference. We use a chrome plating process for standard dies, but for high-volume production (like making sheets for fruit crates), we recommend diamond-like carbon (DLC) coating. DLC is super smooth, too — not just hard. So it doesn’t just resist wear; it also keeps the PP from sticking, which means less buildup that clogs the die. I’ve seen dies with chrome plating warp or develop uneven lips after a year of 24/7 runs, but DLC-coated dies? One client has had the same die for 4 years, and it still makes sheets with consistent thickness. The key here is that smoothness matters as much as hardness — a hard, rough surface will wear just as fast as a soft one, because the rough spots catch on the PP.
Then there’s the roll section — specifically the idler rolls and the cooling rolls. These rolls are what flatten and cool the newly formed PP sheet, and they’re constantly in contact with the solid, warm polymer. The main wear here comes from two places: friction from the sheet moving at high speed (we’re talking speeds up to 100 meters per minute in some lines) and tiny amounts of PP residue that builds up over time. If residue hardens, it can scratch the sheet, which ruins the finished product. So our standard rolls are cast iron, but we coat them with a polished chrome layer for better wear and non-stick properties. For clients making thin sheets (under 2mm) or high-volume food-grade sheets, we offer stainless steel rolls — they’re more corrosion-resistant if we use food-grade PP, and they don’t scratch as easily. I remember a customer who made sheets for bakery trays; he tried cast iron rolls, and the residue scratched the trays, leading to 10% of his product being rejected. Switched to stainless, and rejections dropped to 1%. That’s the quiet impact of wear resistance on quality, not just uptime.
Wait, let’s not forget the less talked-about parts: the gearboxes and the linear rails for the sheet cutting system. A lot of people fixate on the “big” parts, but the cutting blades and the rails that move the die cutter? Those wear out faster than you’d think. The cutting blades shear the hot PP sheet, so they’re dealing with both friction from cutting and heat. We use high-speed steel blades with a titanium nitride (TiN) coating — TiN is gold-colored, by the way, and it’s a staple in cutting tools. Those blades last 3-4 times longer than uncoated carbon steel ones. The linear rails, on the other hand, deal with constant back-and-forth motion, so wear here is from mechanical friction. We use pre-lubricated, hardened steel rails instead of standard mild steel — they don’t rust, and the hardened surface resists the tiny scratches from metal shavings or PP dust that get into the rail grooves. I’ve had a client tell me he changed his rails once a quarter before we switched him to our upgraded ones; now it’s once every 18 months. That’s the kind of small part that can make a huge difference for operators who don’t want to mess with aligning the cutter every few weeks.
Now, let’s get into what affects wear resistance that you might not have considered. First, machine speed. If you’re running the line at 100m/min instead of 60m/min, all the moving parts are moving faster, so friction goes up — that means wear rates can jump 30-40%. Second, PP formulation. If you’re using virgin PP, it’s less abrasive than recycled PP that has dirt, fillers, or leftover additives. I once had a customer who switched from 100% virgin PP to 50% recycled, and his screw wear doubled in 2 months. He didn’t change the screw — but he should have gone for the bimetallic one instead of nitride-treated. Third, maintenance. Wait a second — wear resistance doesn’t just come from the part material. If you don’t lubricate the rails, or you let residue build up on the die, wear accelerates. I see this all the time: a client buys a high-wear part, skips the maintenance, and then complains it’s “bad quality.” We always send a little maintenance guide with every machine, and we’ll walk clients through it over a call, because good maintenance extends wear life by 20-30%, easy.
Here’s the thing that I tell every new customer: we don’t sell you a part that’s “the most wear-resistant” — we sell you a part that matches your production needs. If you’re a small shop making 10 sheets a day, you don’t need a bimetallic screw that lasts 3 years — a nitride one will do, and it’s cheaper. If you’re a big plant running 24/7 for 30 days straight between shutdowns? The bimetallic is non-negotiable. That’s the mistake a lot of suppliers make — they push the most expensive part even when it’s overkill. As a supplier who’s been in this for a while, I’d rather you get a part that fits your budget and your workflow than spend money on something you don’t need.
Let’s circle back to the original question: what’s the wear resistance of parts in a PP hollow sheet machine? It’s not a static number — it’s a balance between material, machine specs, and your own production habits. For the most critical parts (extruder screws, dies), wear resistance can range from 6 months (standard steel, low-volume virgin PP) to 3+ years (bimetallic, DLC coating, high-volume recycled PP). For secondary parts (cutting blades, rails), it’s 3 months to 2 years, depending on the same factors. The key is to not just look at the upfront cost, but the total cost of ownership. A $500 bimetallic screw that lasts 3 years is way cheaper than a $200 standard one that needs replacing every 6 months — that’s $800 a year vs $500, and that’s not counting the downtime.
At the end of the day, I’ve seen too many manufacturers struggle with wear-related issues, and most of the time, it’s because they didn’t match the part to their needs. We’re here to help you figure that out — whether you’re a small business just starting out, or a large plant scaling up. If you’re tired of parts wearing out too fast, or you’re planning to upgrade your PP hollow sheet line and want to pick parts that will save you time and money, shoot us a message to talk through your setup. No pressure, no sales pitch jargon — just straight talk about what works for your operation.
Corrugated Pipe Machine Reference:
Kumar, S., & Singh, R. (2021). Wear behavior of polymer processing equipment components: A review. Journal of Materials Processing Technology, 292, 117058.
Zhang, L., et al. (2019). Coating technologies for improving wear resistance of extrusion dies in polypropylene sheet production. Surface and Coatings Technology, 371, 124-131.
Qingdao Tongsanhegu Plastic Machinery Manufacturing Co., Ltd.
With abundant experience, we are one of the most reliable pp hollow sheet machine manufacturers and suppliers in China. We warmly welcome you to buy durable pp hollow sheet machine for sale here from our factory. Quality products and reasonable price are available.
Address: West of Xixinzhi Village, Sanlihe District Jiaozhou, Qingdao City, Shandong Province, China
E-mail: info@tongsanhegu.com
WebSite: https://www.tongsanhegumachine.com/
